1. Raw Material Warehousing
Precise locking from the source — every incoming lot is quarantined, inspected and released against specification before it enters production.

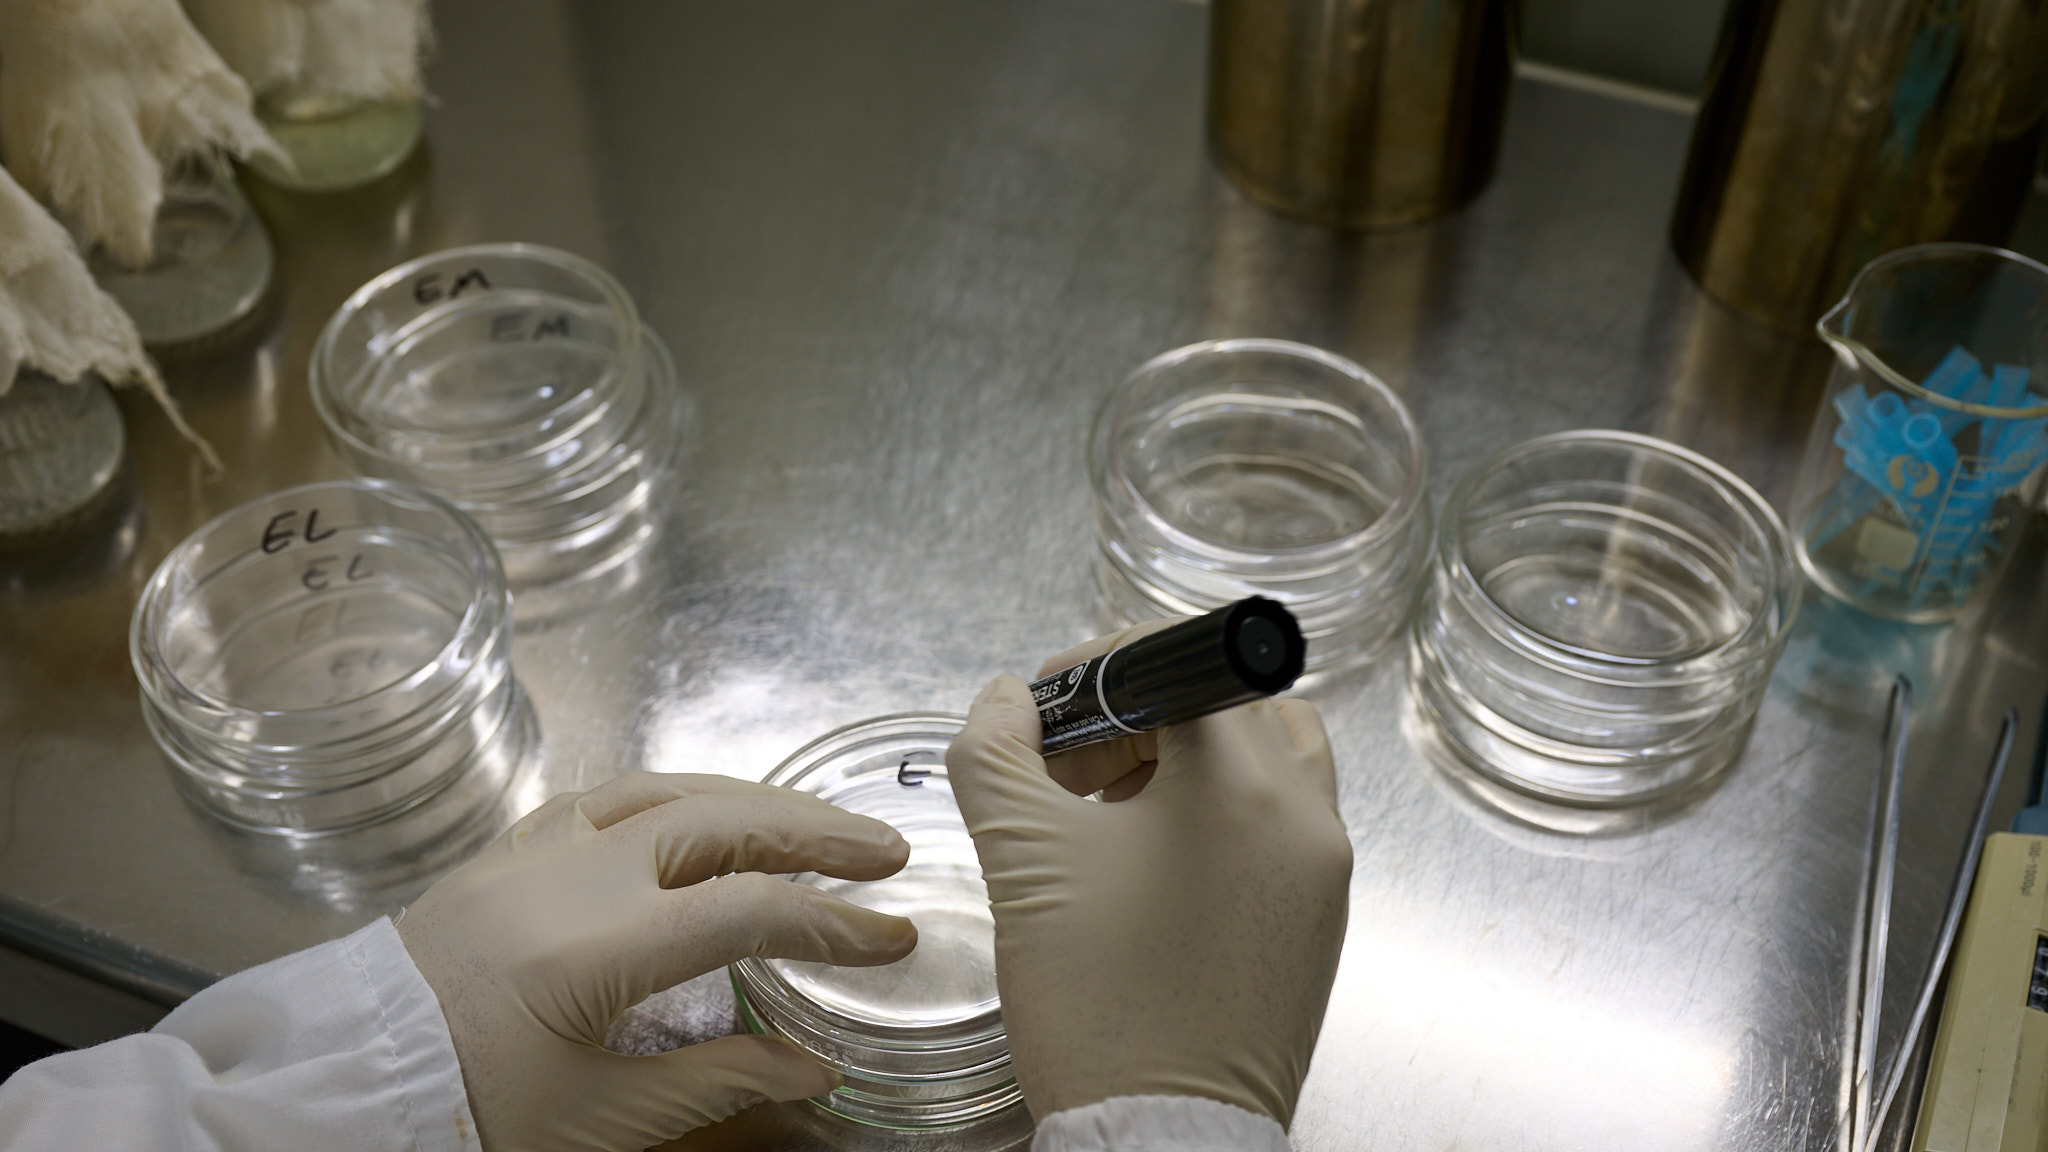
We implement strict quality checks at three key stages: raw material inspection (IQC), in-process control (IPQC), and final product inspection (FQC) to guarantee excellence.
Our well-equipped lab with HPLC, GC, and other advanced instruments allows for rapid and accurate testing, shortening production cycles and ensuring data integrity.
An advanced ERP and batch management system creates a unique identity for every product, enabling full traceability for complete transparency and safety.
3,000+
Batches Inspected / Year
Every Single Lot20+
Test Items per SKU
Micro / Chem / Stability100K
Class (ISO 8) Clean Room
Air Purification100%
Batch Traceability
One Product, One CodeContamination is the leading cause of cosmetic recalls globally. That is why microbial safety protocols are integrated into every production stage rather than treated merely as a final checkpoint.
Our microbiology laboratory conducts total aerobic microbial count and yeast & mold enumeration per ISO 17516, screens for specific pathogens (Pseudomonas aeruginosa, Staphylococcus aureus, Candida albicans, E. coli), and validates preservative efficacy under ISO 11930 standards.
Audited by world-leading inspection bodies to guarantee international cosmetics safety, purity, and global market accessibility.
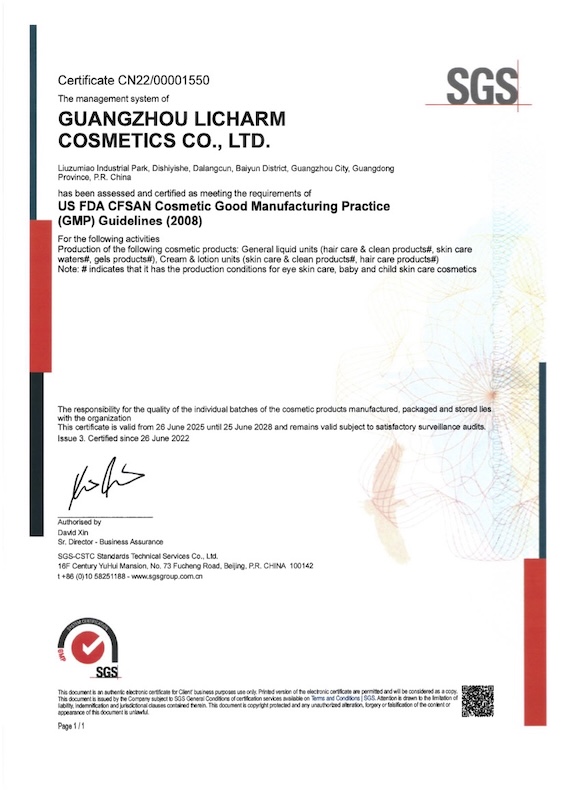
US FDA CFSAN Cosmetics Good Manufacturing Practice guidelines — verified and certified by SGS.
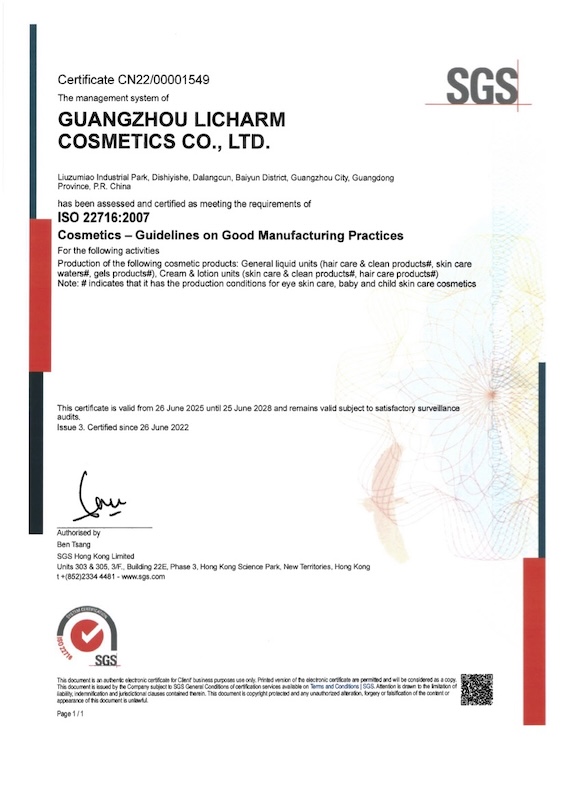
International Cosmetics GMP standard covering production, control, storage, and shipment.
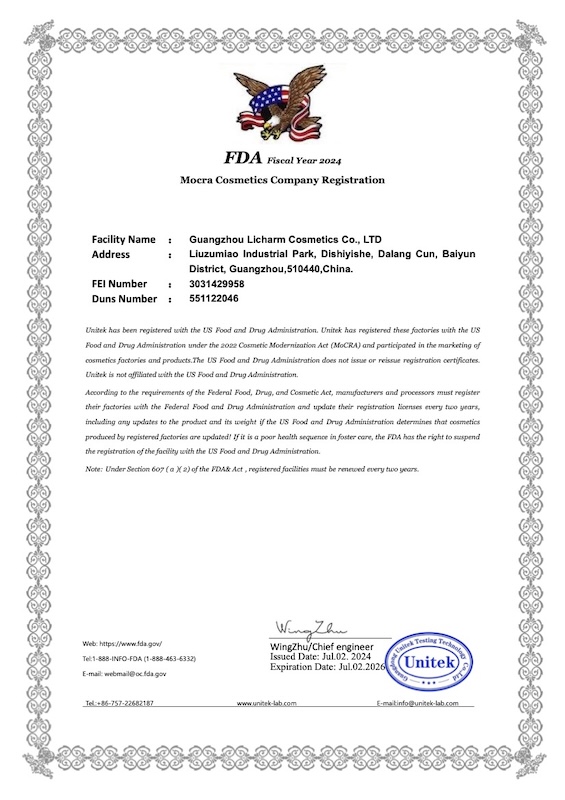
Fully compliant with MoCRA requirements, enabling seamless customs clearance and export to North America.
| 1. Chemical Raw Material Testing | 2. Packaging Material Testing |
|---|---|
| The first line of defense for product safety and efficacy. We have established a full-process monitoring system from supplier qualification to raw material acceptance before production. | Protecting content integrity and consumer experience.We believe the quality of packaging is as important as the product itself. |
| Safety & ComplianceEliminating all potential risks through heavy metal screening, microbial limit control, and irritation assessments. | Safety & CompatibilityEnsuring absolute safety inside and out with content compatibility and harmful substance migration testing. |
| Purity & PerformanceEnsuring every drop is effective via active ingredient analysis and key physicochemical measurements. | Physical & Mechanical PerformanceWithstanding all challenges from factory to use, verified by sealing, physical strength, and barrier performance tests. |
| StabilityGuaranteeing consistency throughout the product lifecycle with environmental simulations and accelerated aging tests. | Functionality & DurabilityOptimizing every nuance of use through component lifespan tests and user experience assessments. |
Precise locking from the source — every incoming lot is quarantined, inspected and released against specification before it enters production.
Recording every detail into our ERP system — enabling two-way traceability from finished product back to raw material lots.
Endorsing quality with data — every product is released with a verifiable "Certificate of Conformity" after passing all QC gates.
Building a solid firewall from our warehouse to your hands — ensuring you receive 100% genuine products through official channels.
Essential answers regarding our analytical testing, clean-room standards, microbial control, and international regulatory compliance.
Yes. LIZEE operates a 6,000 m² certified facilitystrictly compliant withISO 22716:2007 (Cosmetics GMP)andUS FDA GMPC guidelines, covering raw material quarantine, vacuum compounding, clean-room filling, and packaging.
ISO 22716 and GMPC represent the global gold standards for cosmetic safety, hygiene, and batch consistency. ISO 22716:2007 ensures comprehensive quality compliance across compounding, clean-room filling, and storage (mandatory for EU and global markets), while US FDA GMPC enforces stringent microbial limits and sanitization required for North American compliance under MoCRA. Together, they guarantee your products are manufactured in a sterile, legally compliant environment.
SGS is the world’s leading inspection, verification, and testing body, trusted by international health authorities and global retail chains. SGS enforces rigorous on-site audits covering facility engineering, pure water conductivity, microbial limits, and equipment calibration. Holding SGS-audited GMPC and ISO 22716 certifications provides undisputed proof of factory capability, streamlining customs clearance and retailer onboarding for your brand.
Standard testing protocols include microbiological limit assays (ISO 17516),preservative challenge tests (ISO 11930), accelerated stability cycles, in-house heavy metal screening (Pb, As, Hg, Cd), and active ingredient concentration assays via HPLC/GC.
Yes. In addition to our in-house Certificate of Analysis (COA), we coordinate third-party verification and batch testing through accredited laboratories includingSGS, Intertek, and TÜV upon request.
Every lot is assigned a unique batch code in our ERP system that establishes full two-way traceability linking finished units back to incoming raw material certificates, operator logs, compounding tank IDs, and final lab release records.
We perform accelerated thermal aging (40°C / 75% RH for up to 3 months), freeze-thaw cycling (-15°C to 45°C), centrifugation, and light-exposure testing to ensure physical and chemical stability over a standard 3-year shelf life.
Any non-conforming batch is immediately placed under electronic quarantine. We trigger a documented CAPA (Corrective and Preventive Action) root-cause investigation, and no product is ever released until all corrective measures are verified.
Yes. All primary containers undergo formula compatibility screening, vacuum leak tests, torque/drop tests, and pump lifespan trials (500+ actuations) to prevent leakage, material degradation, or clogging.
Yes. We assist with US FDA MoCRA facility listings and product filings, EU Regulation (EC) No 1223/2009 compliance dossiers (including CPSR requirements), and supply batch-specific MSDS/COA documents for customs clearance.
Yes. Retention samples from every manufactured batch are archived in temperature-controlled retention rooms for 3 years (exceeding product shelf life) to support regulatory audits and post-market tracking.